SUPERCRITICAL CO₂ EXTRACTION SYSTEM P-200 – SUPEREX

Origin: Turkey

Brand:

Category:

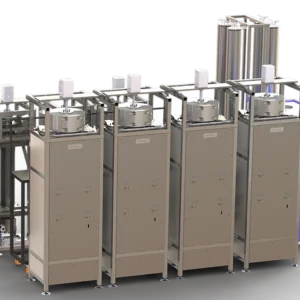
The Supercritical CO₂ Extraction System is an advanced solution for industrial production, utilizing supercritical CO₂ technology for efficient extraction of natural compounds. With a 100L extraction vessel, operating pressure up to 600 bar, and a maximum temperature of 90°C, this system ensures high efficiency and optimized extraction processes. Equipped with a Coriolis flow meter, precise PID controller, and automatic CO₂ recirculation system, it maximizes energy savings with up to 99% efficiency. Additionally, the optional separator cooling down to -10°C enhances compound fractionation capabilities. This is an ideal solution for pharmaceutical, food, and cosmetic industries, ensuring clean, safe, and sustainable extraction.

MODEL: P-200

SPECIFICATION

  • Extraction Vessel Volume: 100 L (or 100×100 L)
  • Special design for efficient industrial production
  • 3 Separators Each with a Volume of 35 L
  • Two separators with pressure and temperature control
  • Separators have interchangeable nozzles for cyclone flow or liquid trap
  • Maximum Working Pressure: 345 bar Maximum Working Temperature: 70°C
  • High CO₂ Flow Rate (10 kg/min)
  • Co-solvent Feed System (1 L/min)
  • Fully Automatic Pressure Increase, Solvent Feed, and Pressure Reduction
  • High-Precision PID Algorithm for Temperature Control Fully Automatic Pressure Regulators
  • Fully Automatic Adaptive Control of CO₂ Pressure and Flow
  • Fully Automatic CO₂ Liquefaction and Recirculation System for Reuse with Efficiency Up to 99%
  • High-Efficiency Heat Pump (COP=6)
  • Increase of the maximum pressure up to 600 bar (test pressure 900 bar)
  • Increase of the maximum extraction temperature up to 90°C
  • Additional extraction vessel with a volume of 100 L
  • Cooling package for the first or third separator (operator’s choice) down to -10°C for more efficient fractionation
  •  Coriolis flow meter by Bass Instruments
  •  Annual Spare Parts and Accessories Kit (ZIP)

PRODUCT VIEWED

The 50L supercritical CO₂ extraction system is designed for industrial production with high efficiency and full automation. The product stands out with its efficient CO₂ reuse, integrated precise pressure and temperature control, and a modern heat pump system. This is the optimal solution for professional extraction applications, ensuring exceptional efficiency and reliability.

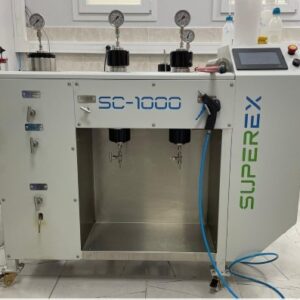
The subcritical water extraction system is designed to efficiently and environmentally friendly extract natural compounds. Equipped with an extraction vessel and two separators, the system operates at high temperature and pressure, allowing for the effective extraction of phenolic compounds without the need for chemical solvents. All surfaces in contact with food are made of stainless steel, ensuring hygiene and preventing microbial attachment. The system features PID temperature control, automatic pressure regulation, and a back pressure regulator, ensuring precise and stable extraction. Additionally, users can integrate a supercritical CO₂ module to expand the extraction capability for high-value compounds.